
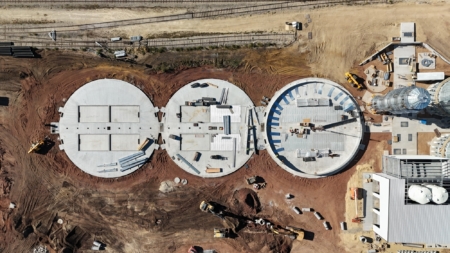
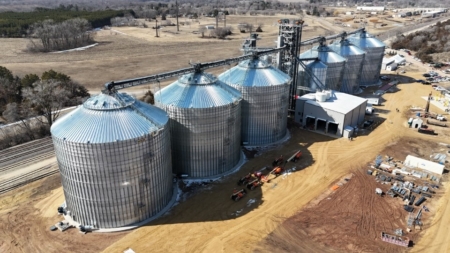
The new ALCIVIA grain terminal in Hager City, Wis. was built to increase receiving capacity, expand storage and strengthen market access for producers in western Wisconsin and southeast Minnesota. The greenfield site gives ALCIVIA direct reach to BNSF, UP and CPKC rail networks and proximity to Mississippi River markets, creating a strategic hub for both domestic and export grain movement.
J&D Construction, Inc. served as the design-build contractor for the project, integrating storage, material handling, safety systems and rail loadout into a unified high-speed terminal.
Structural Centerpiece of the Facility
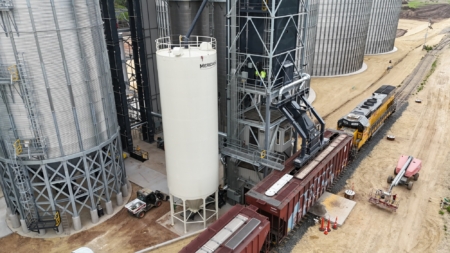
The defining structure on the site is the 20-foot by 24-foot by 151-foot support tower, designed and manufactured by APEX Industrial and installed by J&D Construction, Inc. The tower carries the site’s four main elevators, the 60,000-bph bulk-scale leg, duct distributors and major points of routing for the entire terminal.
The tower includes an enclosed manlift, custom platforms at multiple elevations, a cantilevered platform at the midlevel, and a full stair system running from 110 feet to the tower top. APEX also supplied the 12-foot-wide catwalks connected to the tower, and J&D Construction, Inc. installed all platforms, stairs, bracing, and conveyor supports.
These structures provide safe access to legs, distributors and conveyors without disrupting operations and are engineered for heavy live loads of high-capacity equipment.
Storage and Aeration
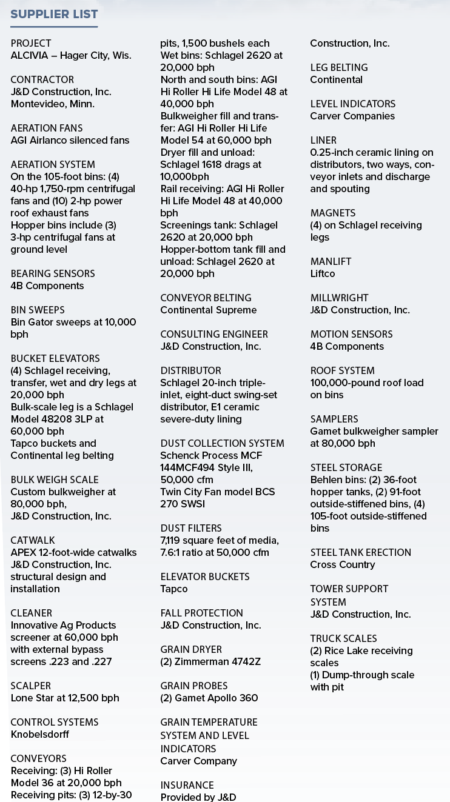
Behlen Manufacturing steel bins erected by Cross Country and supported structurally by J&D Construction, Inc. include four 105-foot-diameter bins, two 91-foot bins and two 36-foot hopper tanks for operational flexibility, blending, or routing segregation. Combined, the structures hold roughly 3.9 million bushels.
Aeration is engineered by AGI Airlanco and incorporates centrifugal fans with silencers, roof exhaust fans and designed airflow-to-static-pressure performance for both corn and soybeans. Hopper tanks use three 3-hp centrifugal fans positioned at ground level. Temperature cables from Carver Industries and level indicators from Carver Companies provide continuous monitoring across the storage system.
All Behlen tanks are engineered with a 100,000-pound roof load rating, allowing operators to support catwalks, conveyors and future equipment modifications.
Receiving, Screening, and Transfer Flow
Three receiving pits feed AGI Hi Roller Model 36 conveyors at 20,000 bph. Grain can move directly to storage, to the cleaning system, to wet routing for the dryers, or into reclaim paths that supply the larger Hi Life conveyor network.
Dual fill paths allow simultaneous loading of wet bins, maintaining dryer supply during peak conditions. When screening is not required, a 60,000-bph bypass path allows grain to maintain full speed through the receiving system. Screenings are routed to a dedicated tank using a Schlagel 2620 drag at 20,000 bph.
Reclaim conveyors include Hi Life Model 48 units at 40,000 bph and Hi Life Model 54 units at 60,000 bph, depending on the route. Hopper tank fill and unload operations are handled by Schlagel drags at 20,000 bph.
Elevators and Conveying Equipment
Four Schlagel bucket elevators rated at 20,000 bph serve receiving, wet handling, transfer and dry routing. A Schlagel bulk scale leg rated at 60,000 bph feeds the bulkweigher and supports high-speed rail loading. Continental belting and Tapco buckets were used throughout the elevator systems. All legs and conveyors include 4B Components motion and bearing sensors for equipment protection and automation.
Reclaim conveyors include Hi Life models rated at 40,000 and 60,000 bph, depending on the path. Dual fill conveyors allow simultaneous loading of wet storage. Hopper tank routing is handled by Schlagel drags at 20,000 bph.
Bulkweighing and Rail Access
The rail loadout system centers on the 80,000-bph J&D Construction, Inc. bulkweigher supported by the 60,000-bph bulk-scale leg. A Gamet sampler provides representative sampling as cars are loaded.
The site’s rail position on BNSF and its ability to load shuttles on UP and CPKC networks expand ALCIVIA’s merchandising reach. According to BNSF, the location provides direct access to western domestic markets and multiple export corridors. Proximity to the Mississippi and Illinois Rivers further enhances routing options when barge freight offers seasonal advantages. Two Rice Lake truck scales, including a dump-through scale with a pit, support high-speed receiving operations.
Dust Control and Safety Systems
Two Zimmerman 4742Z tower dryers provide grain drying capacity for the terminal. Aeration and temperature monitoring across all bins maintain stored grain quality.
J&D Construction, Inc. installed fall protection, tower access systems and structural support across the site. Liftco manlift equipment provides vertical access inside the tower. Knobelsdorff supplied the control system that ties together conveyors, legs, fans, the bulkweigher and sensing equipment.
Dust control is managed by a Schenck Process MCF system rated at 50,000 cfm, supported by a Twin City Fan package and ceramic lining on distributor inlets and spouting.
J&D Construction, Inc. installed fall protection, tower access systems and structural support across the site. Liftco manlift equipment provides vertical access inside the tower. Knobelsdorff Electric supplied the control system that ties together conveyors, legs, fans, the bulkweigher and sensing equipment.
Project Outcome
The Hager City terminal provides ALCIVIA with a high-speed grain handling system designed to meet the needs of its membership and the demands of modern grain marketing. With direct access to multiple rail carriers, river markets, a high-capacity handling system and nearly 4 million bushels of storage, the facility strengthens the cooperative’s position in regional and national markets. The design build approach allowed J&D Construction to integrate structural, mechanical and operational needs into a single cohesive terminal that supports long-term growth and efficiency.